Inside Doc's Machine Shop

Collapse
X
 
  • Time
  • Show
Clear All
new posts

  • DocsMachine
    replied
    Years ago, I had to rob the VFD off of my Arboga drill press, after the old one blew out in my Logan lathe. I later bodged a temporary fix (likely going on it's fifth year ) by just stabbing in a spare WEG.
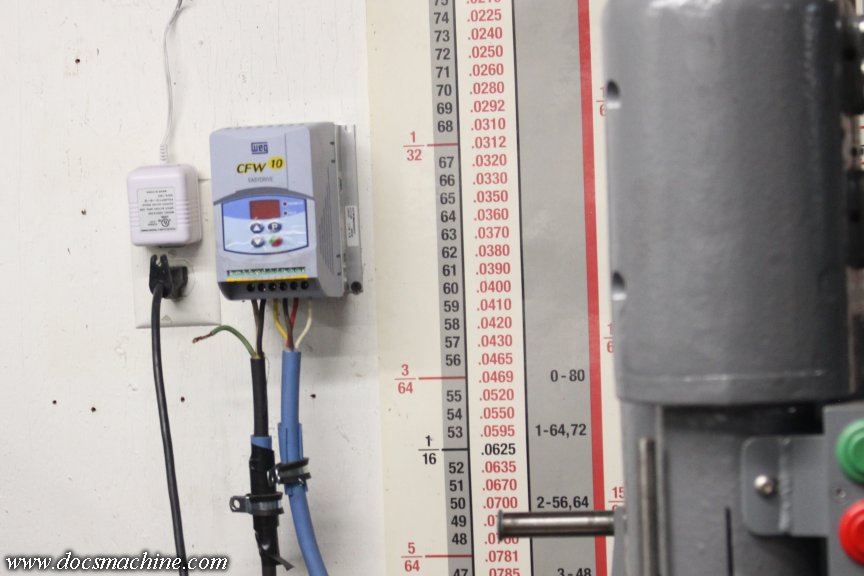


    Problem was, that was only good to 1 HP, and at the high setting, the drill was a 1.5HP. I also never got around to hooking up the stop/start buttons, so it was kind of inconvenient to use.

    Today, as I was trying to make some headway into organizing the bomb crater that is my shop, I ran across the KB VFD I'd bought... three years ago? Specifically to install on this machine. I'd just put an identical one on my buddy's Scotchman saw a few months ago, so I had extra switches and cable piled near it.
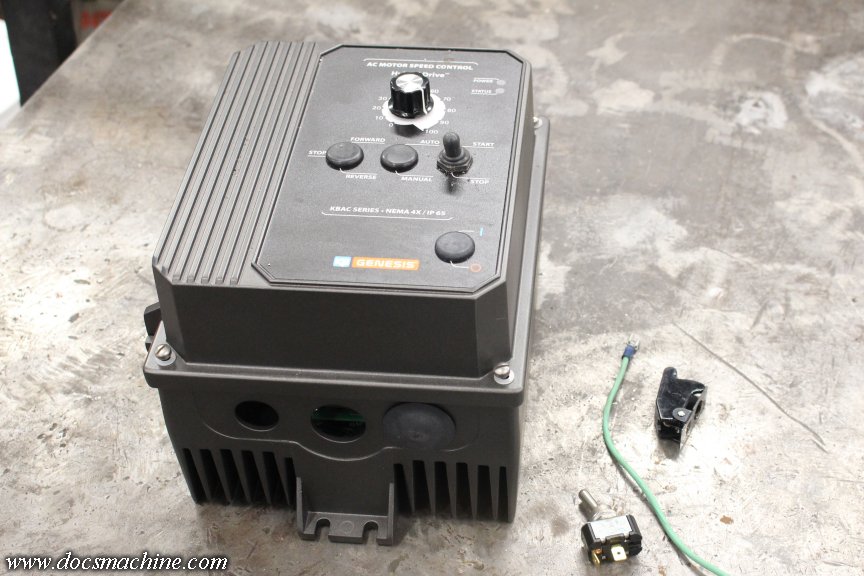


    So, since I had a freshly-cleared off workbench, and I was getting tired of just moving stuff from one random pile to another, I dusted it off and started taking stock of what I had, and what I needed to do.

    The big trick here, and has been since I got this drill a decade and a half ago, is to actually mount the VFD on the machine itself, rather than screwed to the nearest wall. The design of the drill doesn't give me too many options for mounting, though. I didn't want to put it down by the base, since the VFD has a power switch on it, and I wanted that and the speed control easily accessible. Ditto mounting it on the back of the column, facing away.

    So more or less since the beginning, I've been toying with the idea of mounting it to the top of the column.
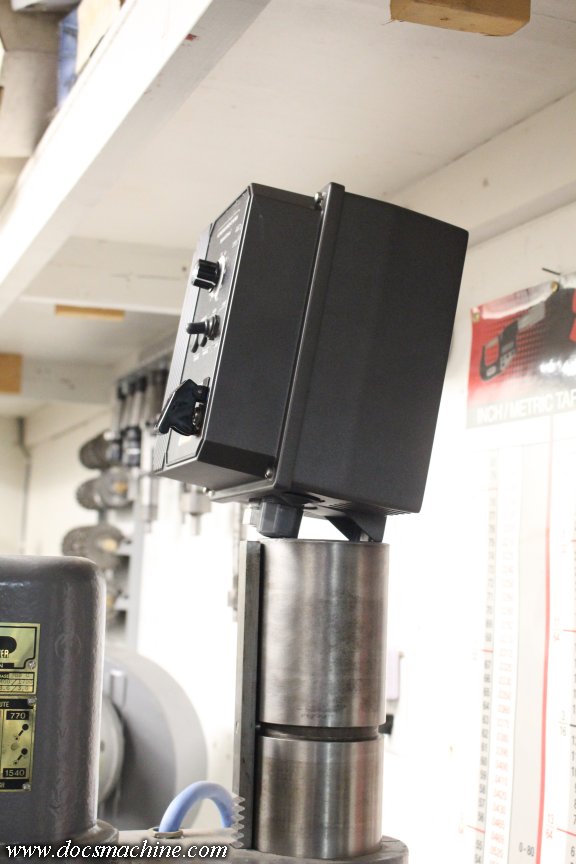


    Some sort of L-shaped bracket that bolts to the top of the column, perhaps... I have a couple sketches, but I may need to do some cardboard mockups. For example, the large middle boss of the VFD is where the heavy 3-phase cable comes in from the motor. I can't have that too low to the column, or the VFD too far forward, since the head can be raised on the column and could interfere.

    On the other hand, the original design for this machine was the power cord came up the center of the hollow column, to connect to the controls. I'd like to do that to the 220V 1Ph feed to the VFD. There's a 'port' in the drill's base casting specifically to run a power cord into.

    But, that's all for another time. I still need to get the whole shop into some semblance of 'tidy' and get the Capital-F back to work. So in the meantime, I prepped the VFD by first adding a cutoff switch and another one of the military-style switch protectors, just 'cause it's cool...
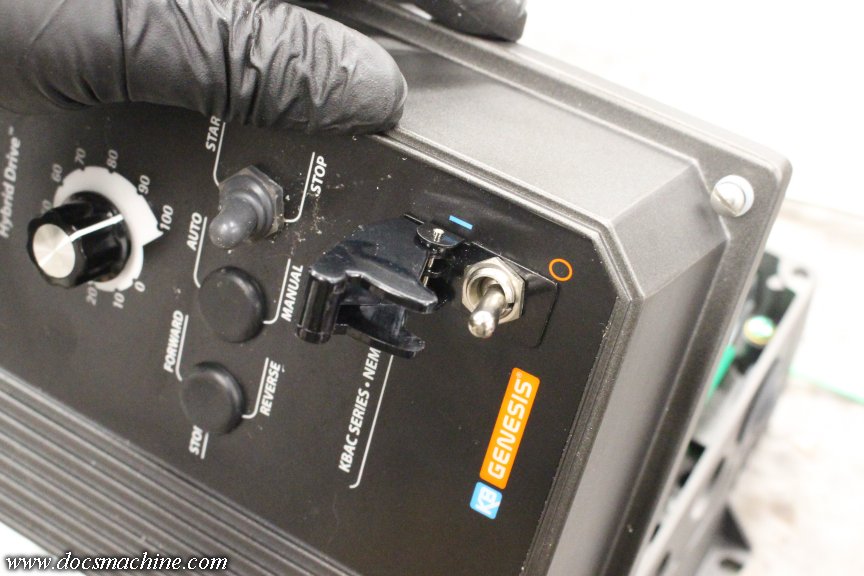


    Then removed the start/stop switch, and corked the hole with the freshly-removed rubber plug from the power switch port. The buttons on the front of the drill press will do the start/stop, so no need to have it on the VFD.
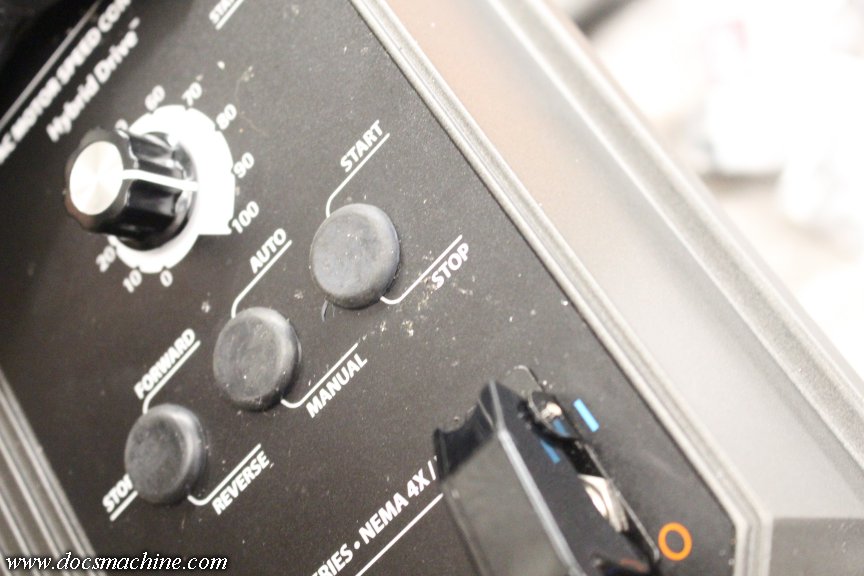


    Stripping nearly a foot from the end of some 300V cable, I got the new power switch wired internally, and locked in with a weathertight gland.
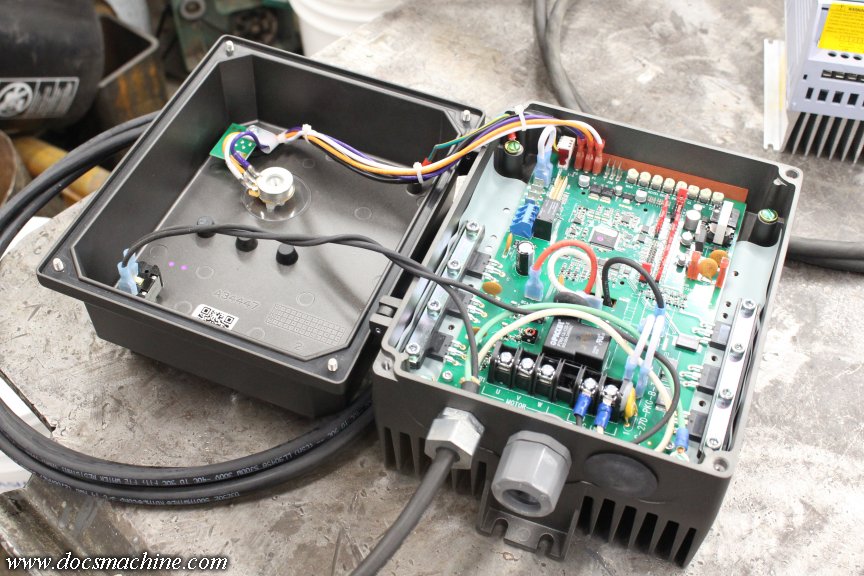


    ... Aaaand, that was about as far as I could go today. Next step, whenever that may be, will be to fab a mount- that's the tricky part. After that it's just wiring. Mostly.

    Doc.​

    Leave a comment:


  • DocsMachine
    replied
    A close call for Christmas, but Santa delivers! (And, a good illustration of why Doc is so hard to buy for. )

    I'd actually ordered two different 1-1/4" boring bars back when I got the rusty one- but that one came Priorty, and this one came, I'm guessing, by dogsled, presumably pulled by arthritic corgis or something. The first one I got in part due to it being bundled with a now-rare 1-1/4" CXA toolblock, but this one is the better of the two bars.

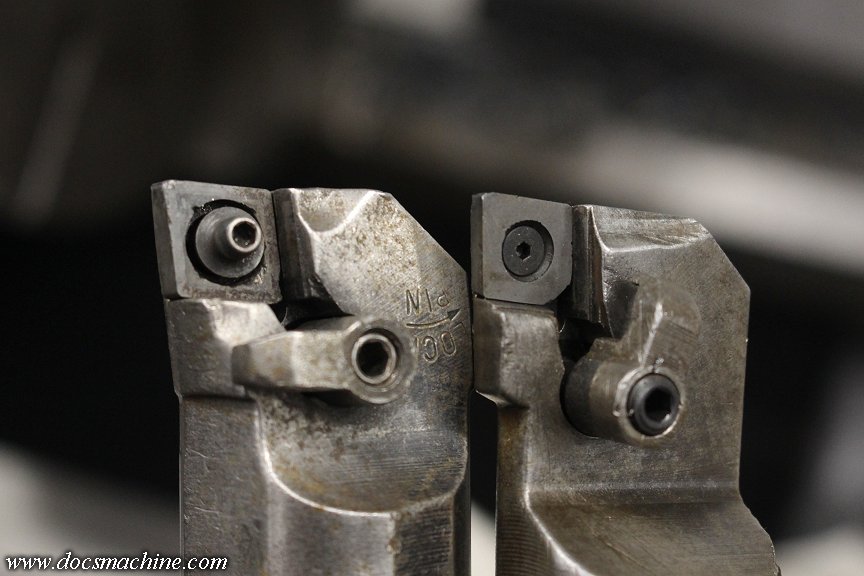
    They're both Kennametal, but the latest one is a newer generation:


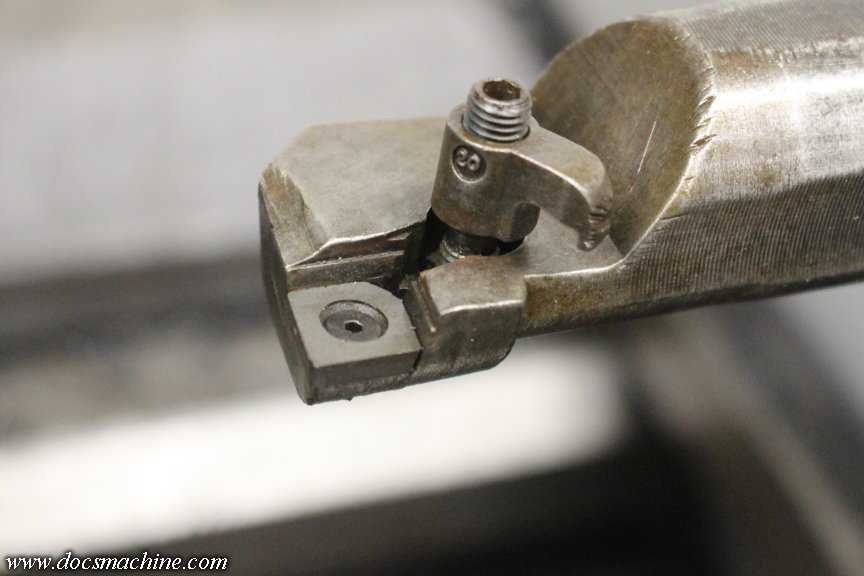
    I have no idea when the changes were made- the older one could be 50-60 years old. But there's a couple of improvements: First and foremost, that center "pin" on the left-hand one (the 'newer' one) is a secondary retention for the insert. And second, how the reduced end of the bar on the newer one is both shorter and thicker- less metal was cut away. That makes for a stronger overall tool, with a better-retained insert.

    That center pin is machined eccentric, and is turned to help lock the insert into its seat. (Note the arrow.)


    The other bar is still a good, strong tool, but this one will be better for the really heavy-duty turning.

    Also, I was lucky enough to find a second 1-1/4" tool block, giving me two complete setups.


    I'm still going to need a good 1" bar, and possibly a dedicated 3/4" bar (not one borrowed from the Omniturn ) but those will come later.

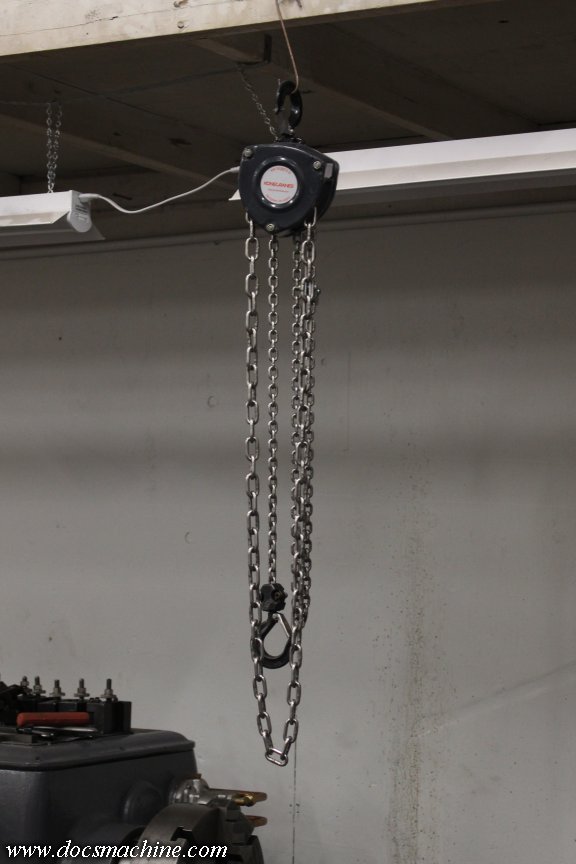
    Also, I splurged on a cute little 1/4-ton chainfall, that also finally came in:


    So here in the hopefully not-too-distant future, I'll pick up some rollers and Unistrut, and get to designing that overhead trolley to lift, move and carry the chucks, and if necessary, heavy workpieces, too.

    So... yeah. Shop toys I don't quite get to play with yet.

    Merry Christmas!

    Doc.​

    Leave a comment:


  • DocsMachine
    replied
    As we were talking about big boring bars earlier, during one such conversation, I idly checked eBay and almost immediately ran across a combo deal in my price range.

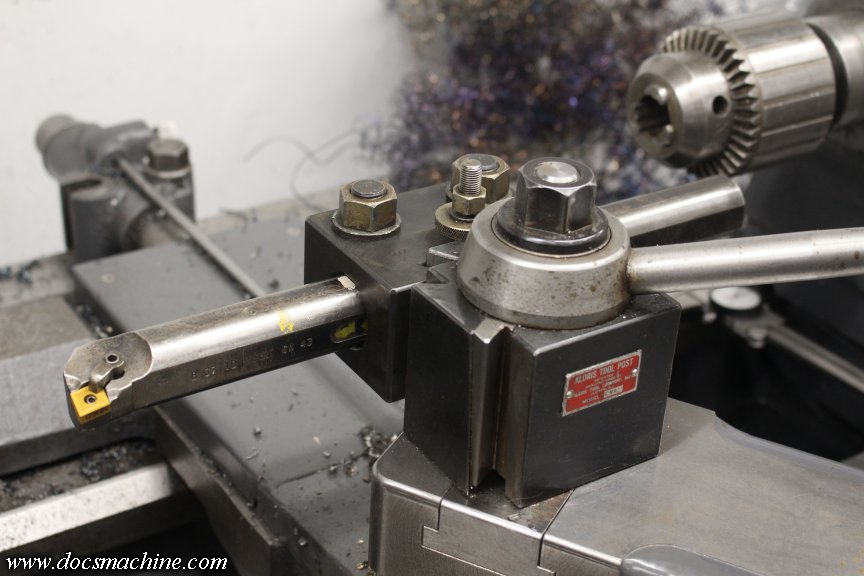
    A Kennametal CNMG 1-1/4" diameter boring bar, with a hard-to-find Aloris CXA tool block that takes 1-1/4" bars. (Aloris only sells CXA blocks for 1" bars, today.) It was rusty and well used, but the seller was asking right about what the tool block itself usually goes for.

    Even though finances aren't as flush as I'd like them to be, and I have no plans to do any heavy turning like that again in the near future... well, I'm still a tool geek at heart so I hit the BIN button.

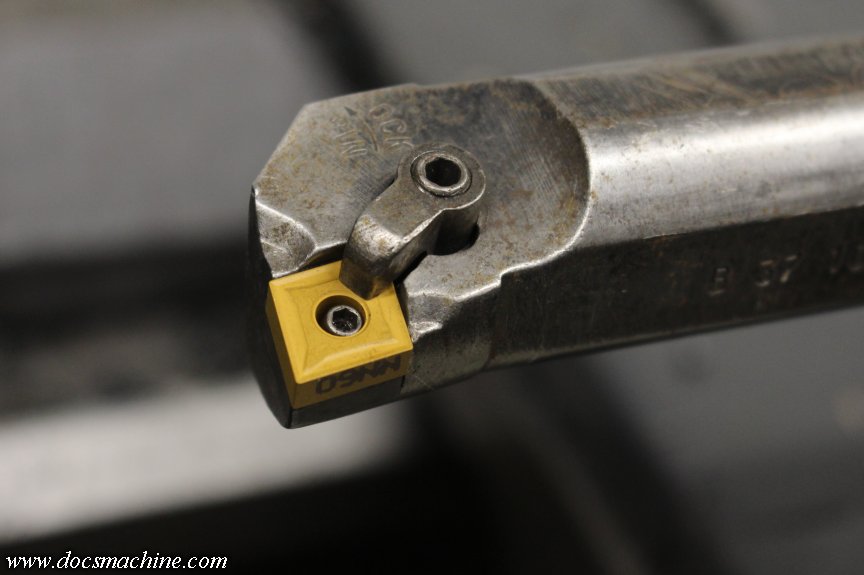
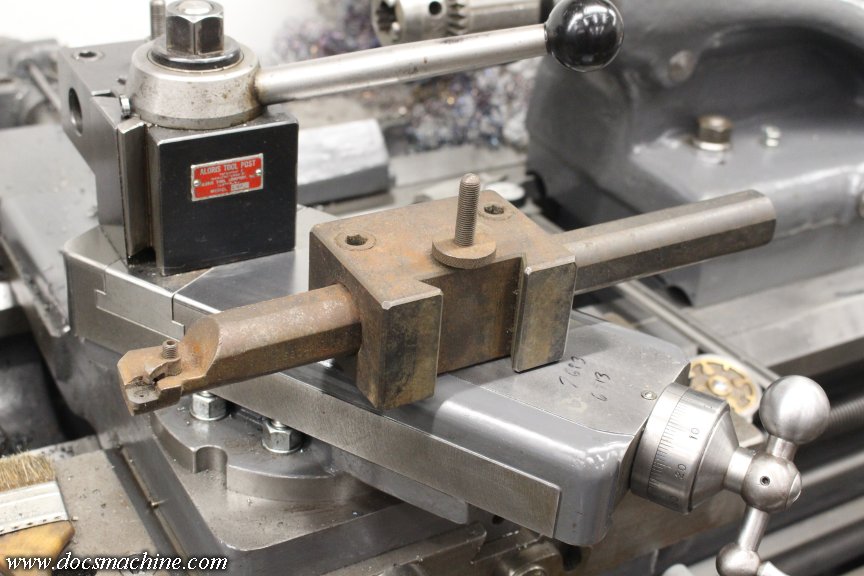
    Here's what I got:


    It's not as bad as it looks. It's light surface rust, and only on the upper surfaces, so that tells me this spent some time in an unheated shop for a while- and overall, likely hasn't been used in many years.

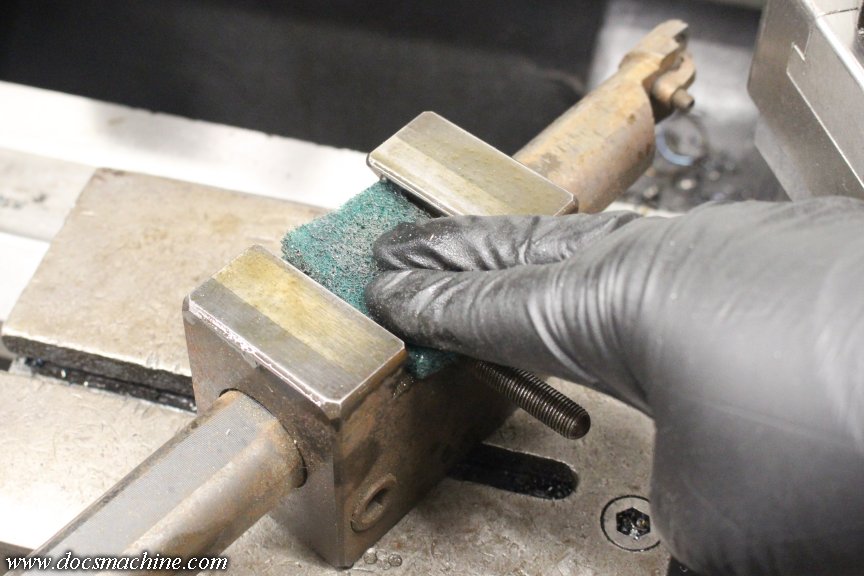
    So first, I hit the mounting dovetail with some Scotchbrite and WD-40...


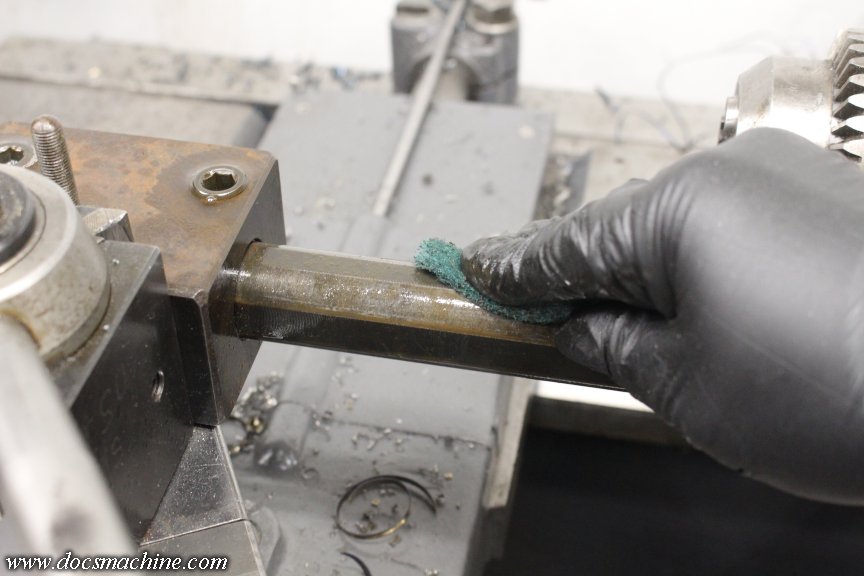
    ... So that I could mount it in the toolpost and break the clamping bolts loose. But first, I also scrubbed the rust off the shank of the bar...


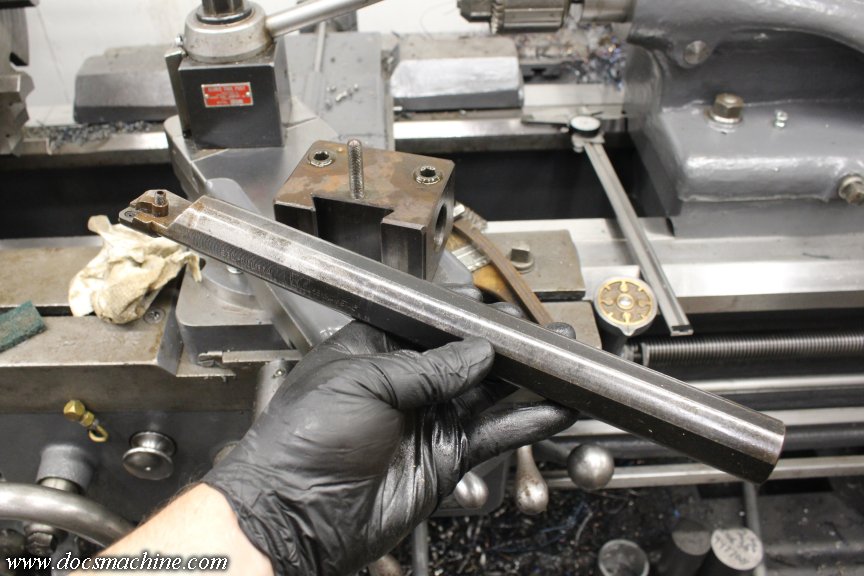
    And once the locks were loose, she slid right out.


    A little more scrubbing and wire brushing got almost all the rest of the rust off, and a similar scrubbing on the tool block cleaned it up, too. Neither will ever look "new" again, but that's all right.

    ... Maybe I'll degrease 'em and try some gun blue.

    The nose of the carbide seat/anvil was, as is so typical, cracked off, so I simply reversed it. I have some new ones, but might as well use this one up before slapping one of those on.


    And, here's where things went sideways. The hex inside the clamping screw was almost completely stripped out.


    It had just enough grip to kind of seat, but wouldn't hold the wrench to loosen. I had to grab it with a vise-grips to get it back out.

    Those I don't have a replacement for. If this was a time-crucial job, I could rob it from one of the square-shank tools, but in this case, I just ordered a two pack off eBay again.

    Toying with the idea of getting the later model clamp, too, that has a longer nose and a pin that hooks that center hole. Not 100% sure it's compatible- this is a long-obsolete model of bar, but I may try. There's also a later style of pin that holds that lower anvil, and helps retain the insert through that same center hole. This bar wasn't designed for it, but if I can find an appropriate size pin, I may redrill and tap for it, to add the extra security.

    But, overall, it cleaned up nicely, and I have no doubts it'd do another job like I just ran, with aplomb.

    Doc.​

    Leave a comment:


  • DocsMachine
    replied
    Got it, my mistake. I was referring to lucrative in reference to finances, not availability of work.
    -I blame the manufacturers. They need to go back to making crappy, unfinished guns like they used to do. The old Shockers that didn't have an "off" switch, 'Cockers that needed to be completely rebuilt before they were "tournament ready", 'Mags and Angels that "needed" a bunch of aftermarket parts...

    Nowadays, everybody just pulls an Emek out of the box, screws on a tank and hits the field. What's a poor, down-on-his-luck airsmith to do?

    Doc.

    Leave a comment:


  • StaticShocked
    commented on 's reply
    Got it, my mistake. I was referring to lucrative in reference to finances, not availability of work. I misunderstood.

  • DocsMachine
    replied
    I don't think any type of metalworking is lucrative.
    -Er... Everything uses some form or another of metalworking. Cars, computers, TVs, cell phones, beer bottles, beer cans, airplanes, wristwatches, houses, lawnmowers....! Even carpentry needs metal nails, saws and hammers.

    What I meant is what I said- this airsmith thing isn't all that lucrative. I mean, I do what I can, but this market just isn't that big. I'm a niche maker for a niche segment of a niche market.

    Doc.

    Leave a comment:


  • StaticShocked
    commented on 's reply
    Aloris tool posts are so nice. Definitely my favorite lathe tool post. I have found some of the off-brand ones are getting quite good nowadays.

    If you could get the encoder on the inside, that would be so neat. It would be free of chips and the potential damage from being on the outside (even with guards). That would be a really clean install and the ideal location. I have made a few custom components just to ensure the encoder and scale are mounted on the back, out of the way and protected, but DRO's on the inside of the saddle would be the ultimate location. If you end up doing it, I look forward to your write up on the install!

    Sweat equity is the way. I don't think any type of metalworking is lucrative. It seems rather like long hours and demanding customers who want the impossible because someone told them it was possible?

  • DocsMachine
    replied
    We have been buying a lot of boring bars (coincidentally, CNMG) and allied spade drill holders from eBay recently to surprisingly great success.
    -I buy a lot of tooling off eBay. Best place to get lightly-used stuff, or even heavily-use-but-still-serviceable.

    Since I finished those parts, I found what's probably a Kennametal boring bar on eBay, along with a CXA tool block. Aloris doesn't make a CXA block that takes a 1-1/4" bar, so presumably somebody bored it out.

    The set is used and a bit rusty, but of course both are just blocks of solid steel- and I know how to cure rust. And given my budget, the fact that both together cost less than a lightly-used CXA block alone.


    Also, we are really fond of the Newall brand of DRO's.
    -Been wanting a Newall since the days of the old Enco catalog flyers.

    But we're back to that budget thing- a good Spherosyn kit was well over $2,000, and I'd wager a 3-axis is closer to or over $3K today. That's just been more than I either want, or, more commonly, even have, to spend.

    Though I have spent a little time considering that it may actually be possible to fit a Microsyn encoder inside the big Springfield saddle. I wanted to do that back when I was still reassembling the beast, but there was just no way I could blow that much cash. (This airsmith thing ain't as lucrative as it looks- I have a nice shop, but it was 80% paid for with sweat equity. )

    Doc.
    Last edited by DocsMachine; 12-04-2025, 03:03 PM.

    Leave a comment:


  • StaticShocked
    commented on 's reply
    Getting a machine all setup and efficient is so satisfying. Glad to hear the hot weekend job went smoothly.

    We have been buying a lot of boring bars (coincidentally, CNMG) and allied spade drill holders from eBay recently to surprisingly great success.

    Also, we are really fond of the Newall brand of DRO's. They are an English company owned by Sansata i think, and we have found the DRO's to be bullet proof (not literally). Very happy with them after almost 15 years of using them. DP700 is on most manual lathes and mills and DP1200 on the big boring mill. They even have hole patterning / basic repeating capabilities for slots and such to make repeat machining easier. The main thing for me was the linear scales a very durable. Leave oil on them, coolant, chips, blow it all around with air, whatever, they keep working (unlike glass scales...).

  • DocsMachine
    replied
    So, after all this, what have I learned?

    Mainly that I need more tools. Duh!

    This machine really needs a DRO. I've been pondering getting one for it and another for the Sheldon, but I've never liked how they take up room on the side of the cross slide, since at least on the Sheldon, there isn't that much quill travel to start with. And on the big Springfield, it'd need heavy armor to protect it from getting crushed up against the tailstock base.

    I also need at least two of my own heavy boring bars. Most of what I have takes HSS, and anything that takes an insert is only 3/4" on the shank. I need a good name-brand 1" and probably a 1-1/4", that take a heavy insert, like a CCMT or a WNMG.

    I should make a mount for the bigger bars I already have, too.

    I need to fix that micrometer stop. I knew it was going to be an issue a decade ago when I first fitted it to the machine (it's actually, I think, a Mori-Seki stop) and have meant for years to either re-etch or replace the knob. It has a 20TPI thread, so it could easily have 50 .001" graduations. Needs a spring or something to give the barrel a little friction, too, it turns too easily.

    I did manage to find an original Springfield carriage stop, but the screw and dial on that were badly damaged and also have to be replaced.

    I need a worktable or cart I can roll up to this thing. I had tools piled on the bed, on the floor, on the gearbox, on the headstock and on the bandsaw table.

    Going along with that, I need to make a tool shelf bolted to the wall for this thing, somewhere. And along with that, I have the "tool stand arm" or whatever they call it, for this thing, that bolts to the back of the bed. I need to make a new top plate for that, to keep the occasionally-used tools on hand. The oil can, drill chuck keys, drills, etc.

    And the big one: I really need to put together the overhead trolley system I've been thinking about since I got this machine back together. The 8" and 10" 3-jaws aren't too big a deal, but the 12" 4-jaw, especially leaned out over the bed of a large lathe, is a pain in the sphincter to install or remove.

    And the 15" 4-jaw is basically impossible without an engine crane. The 86 pound slug of steel was no picnic either.

    I have in mind a trolley made out of Unistrut, with maybe a 1/4 ton chainfall, and a heavy steel rack behind the bed, or maybe at the end of the bed, to hold the chucks. (At least the big ones I can't easily manhandle into place.)

    Now, I've known most of these issues for years, but I use this big machine so relatively rarely, that other needs in the shop tend to take understandable precedence. That said, this job would have gone a lot smoother with those things, and hey, if I'm going to have this six thousand pound monster in my shop, taking up as much room as a small car, I might as well have it capable of doing the jobs it's... well, capable of.

    ... Well, that was a nice bit of fortuitousness. Just checked eBay and spotted a 1-1/4" boring bar, looks like an older Kennametal, that takes what appears to be CNMG inserts, with an Aloris CXA tool holder block. It's all a bit worn and rusty, but the price is right, and I know how to deal with rust.

    Doc.​​

    Leave a comment:


  • DocsMachine
    replied
    And DONE, with a day to spare!

    I did all the above on the 26th, and after the food coma wore off on the 27th, I went out and made the last few passes to bring it to size.


    It was better in any case that I gave it time to cool down before trying to cut to spec. After I was done boring, the thing was over 200°F, according to the infrared gun. And it's big enough that had I cut it to spec at that point, it would have cooled off to potentially out of spec.

    When I went to start cutting it cold, I was wondering about that, so I took an .005" skim cut, just out of curiosity. Turns out the OD was both out-of-round, but also tapered- it was narrower at the base, where the thickest part of the metal was. Fortunately I'd left .100" for that reason, and a few light, slow passes brought it back into shape.

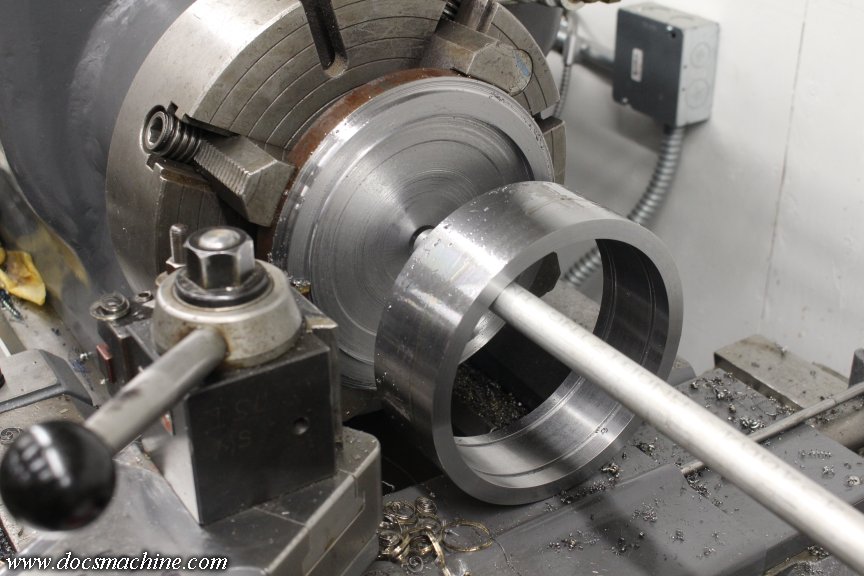
    Then, I parted it off, slowly and carefully- with a rod held in the tailstock drill chuck to keep the ring from rolling about and maybe getting dented.


    We're not quite done with that, but there's still the second one to do, which I started on the morning of Black Friday. (Nobody around here has 'doorbuster' sales on lathe tools or endmills, so why bother shopping? )

    This one was the larger of the two- roughly eighty-six pounds and about as much as that 12" 4-jaw can hold. I have a 15" 4-jaw, but I need the engine crane to mount it.


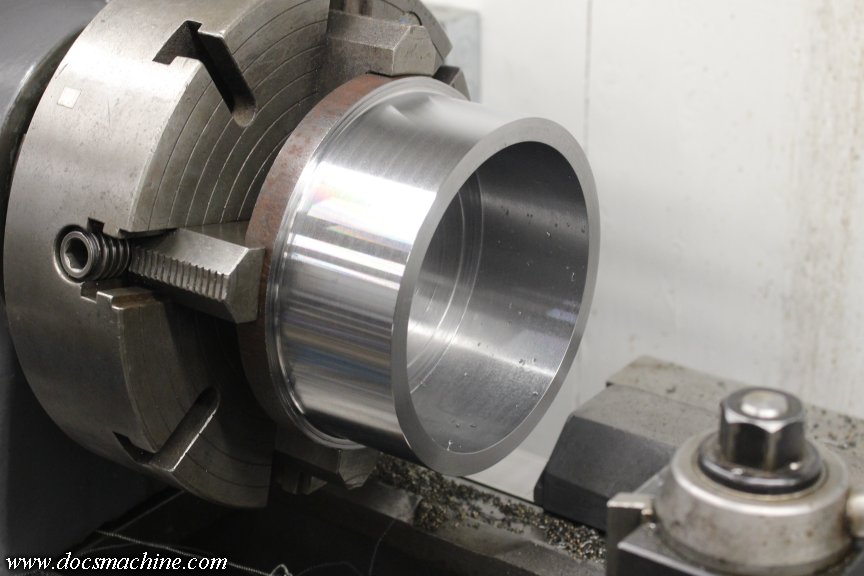
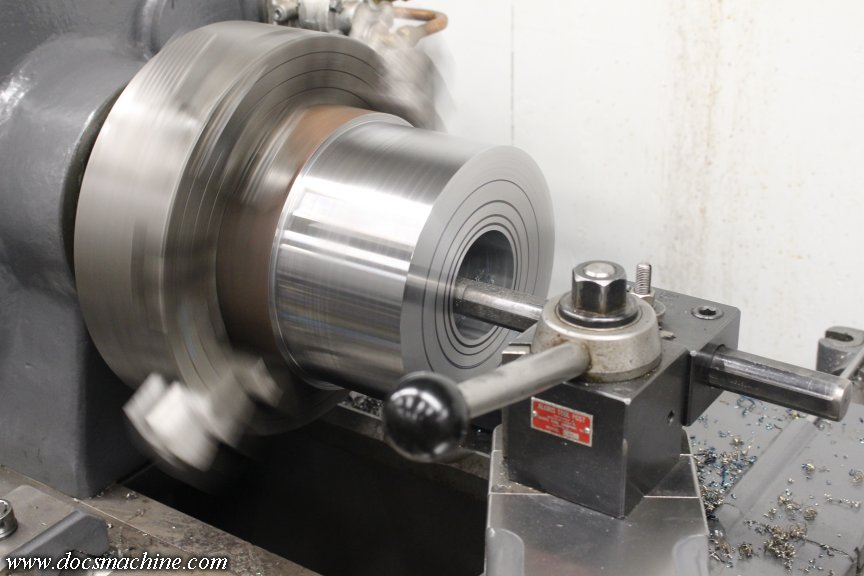
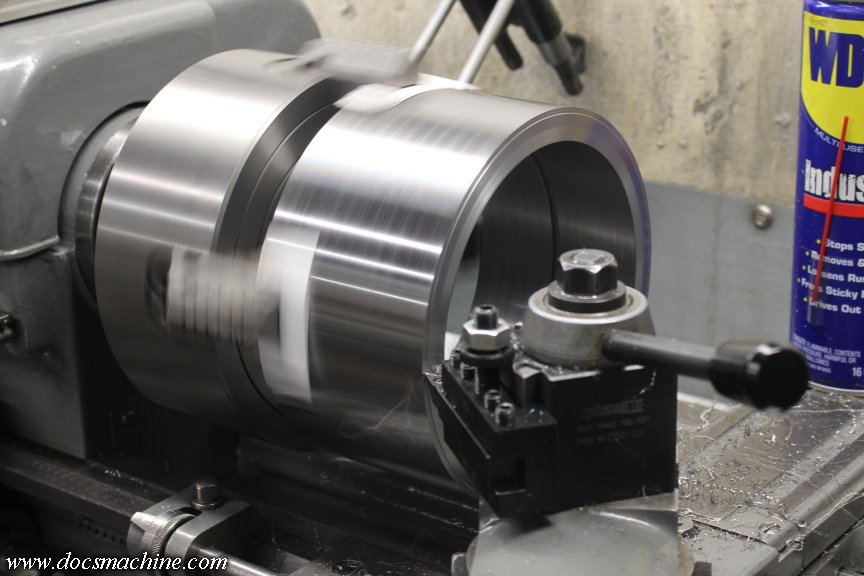
    But, same operations. I got it faced, roughed to the OD, and drilled, then today (Saturday) I got the rest bored out:


    The black rings are just pen marks, gives me a better idea of progress since I can make eight or nine passes and the center doesn't seem to get all that much bigger.

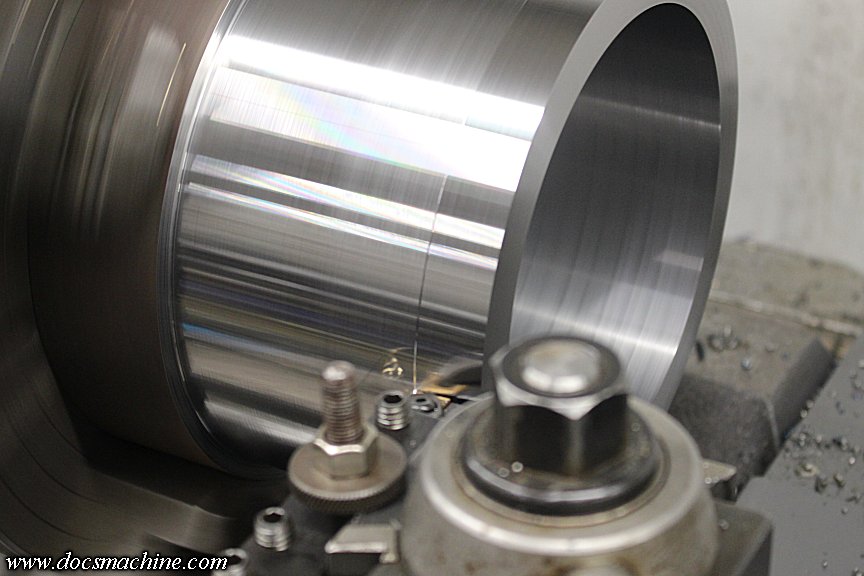
    But, eventually we got down to the finish pass here, too:


    And once the internal O-ring grooving was done, I parted this one off, too.


    Captured by the drill chuck directly this time.


    I used the smaller Sheldon lathe to face the parted end to length, mainly because that thickness was a tight tolerance, and the Sheldon has a better micrometer carriage stop.


    The big Springfield has a micrometer carriage stop, but the dial is for some reason marked on .0025" increments, and indicated in round numbers. That is, 0 to 1 is .0025", 1 to 2 is .005", 2 to 3 is .0075", 3 to 4 is .010", and so on. I can make it work if I have to, but as a last step on a part I've spent two days on, is due in another day, and cost $150 just in steel? Nope, I know and trust the Sheldon's stop.

    (I've been meaning to make a new dial, or recut some new marks... along with all the other things on my to-do-list...)

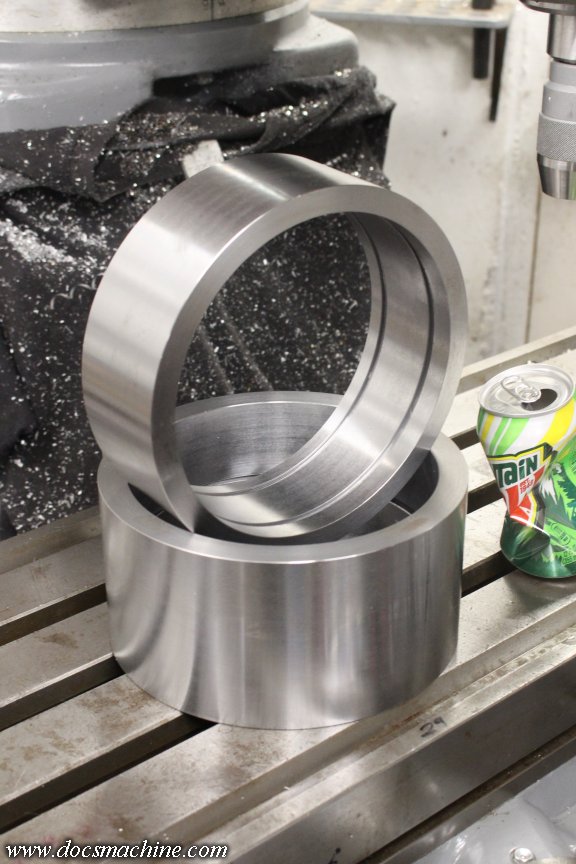
    And done! With a full day to spare!


    Yeah, finished they don't look like much, but due to the size, they had to be cut from solid, and due to the use, they needed to be tough chrome-moly.

    And since it's the oilfield, they had to have 'em, and were willing to pay for it. (Well, at this point I sure hope I get paid... )

    Doc.​

    Leave a comment:


  • DocsMachine
    replied
    While I don't generally do "job shop" work- I have, but it's often proven more trouble than it's worth- I had a case where a good friend needed a time-sensitive job done. And, as a rare treat, no issues with how much it's gonna cost- they need the part, the company will pay.

    That's not to say I have carte blanche to pad the bill- I don't do such things- but it's case where, when I tell the client an estimate of the cost, they don't say "well, I was hopin' to only spend this much" or something similar.

    Which is a good thing, because this is a big job- at least for me.

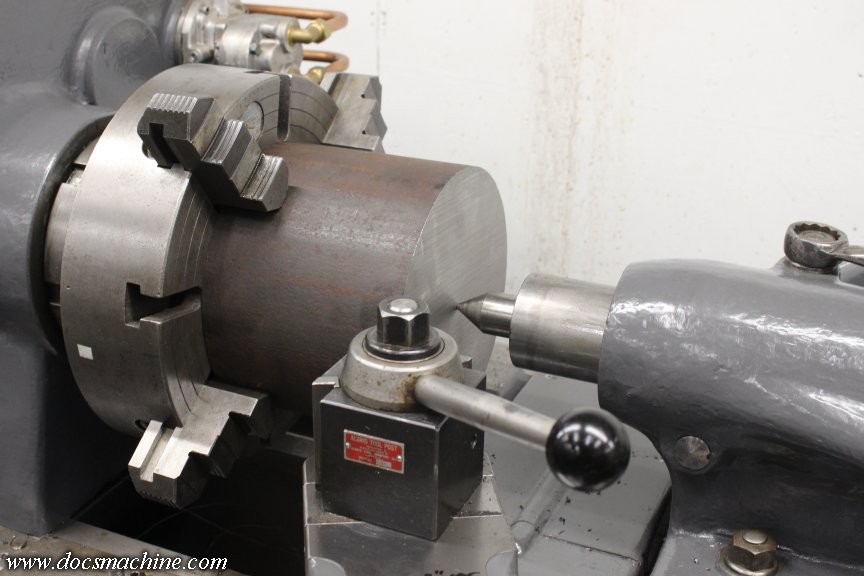
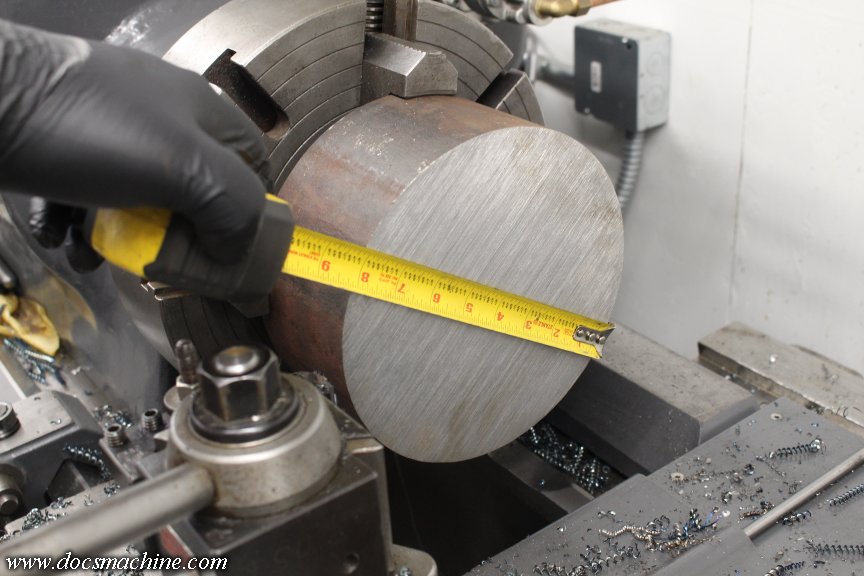
    First, we started with an eight-inch, fifty-pound slug of 4140 chrome-moly steel:


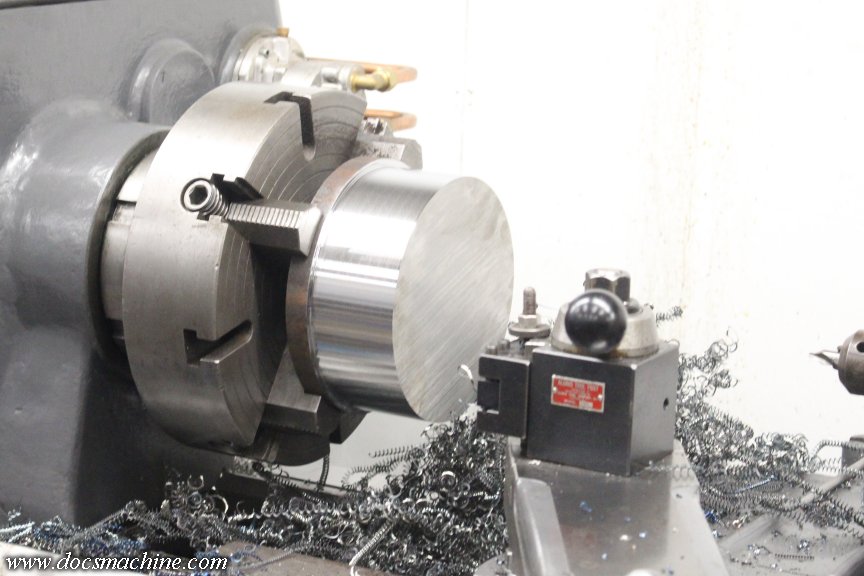
    The OD gets buzzed down to 7-1/2"...


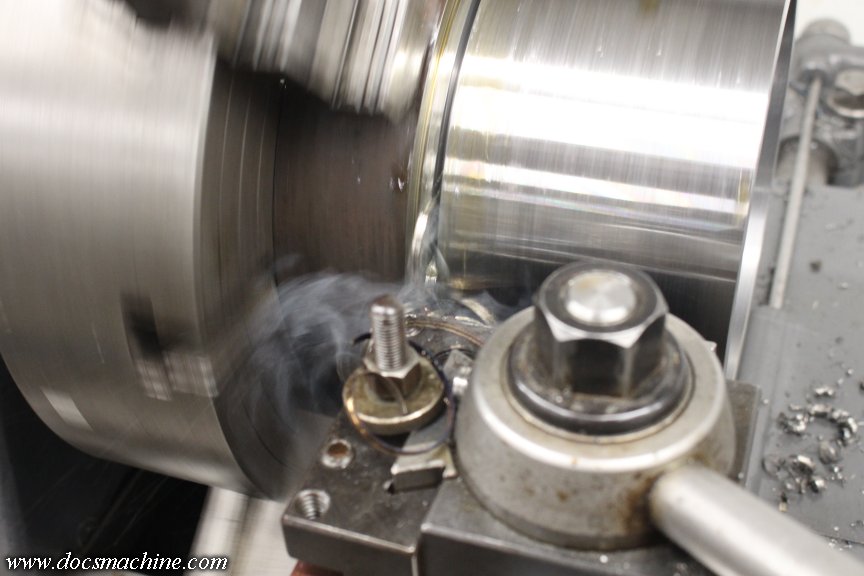
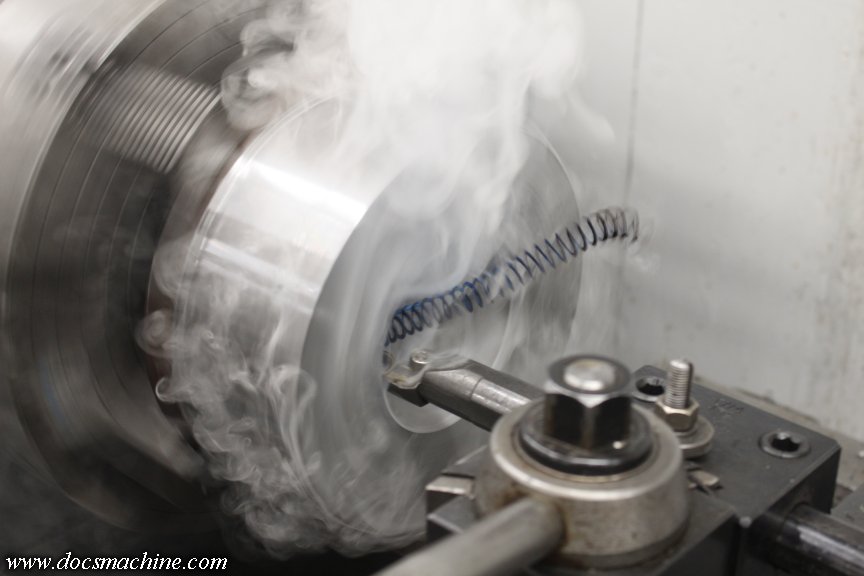
    "Buzzed", in this case, means an hour of heavy turning at 120 RPM on a 10HP machine, with blue-hot swarf flying off.

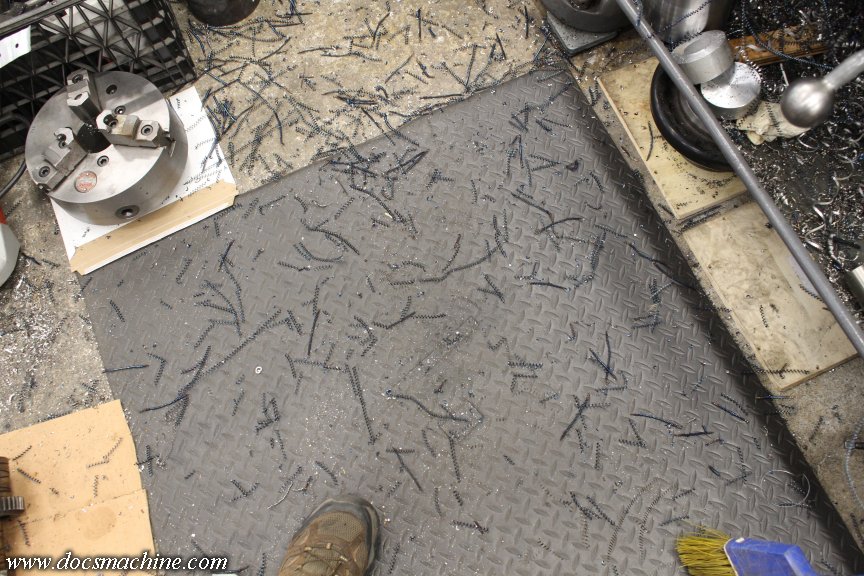
    See all those little springs?


    I can't sweep those off. They've partially melted into the rubber mat.

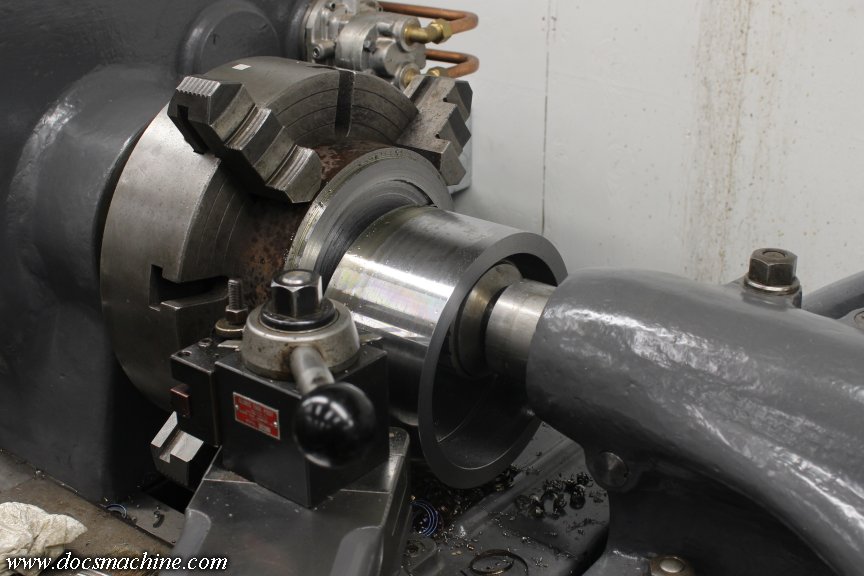
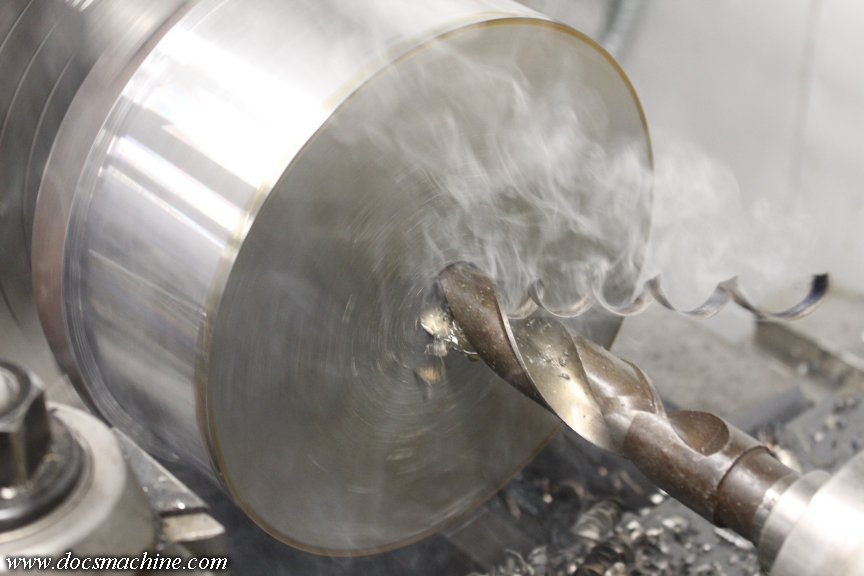
    But now for the fun part. Drilling out up to a 1" pilot hole...


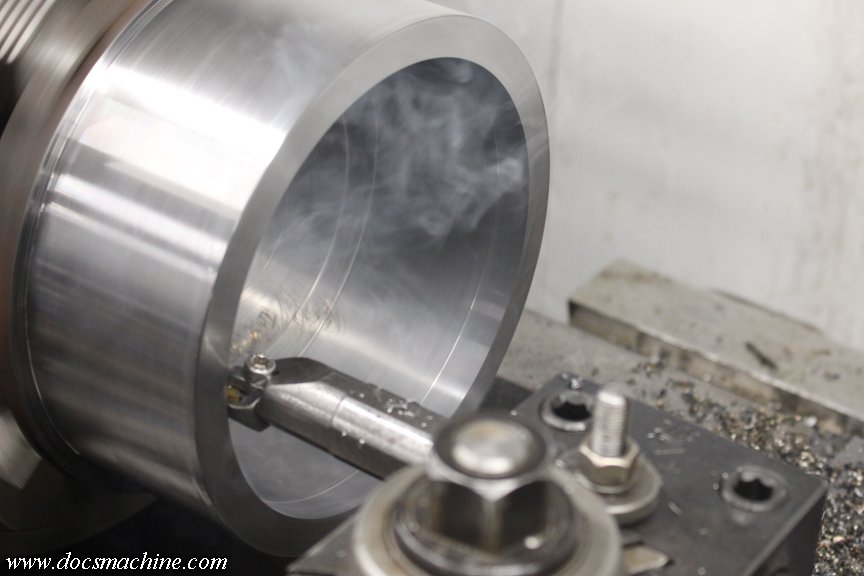
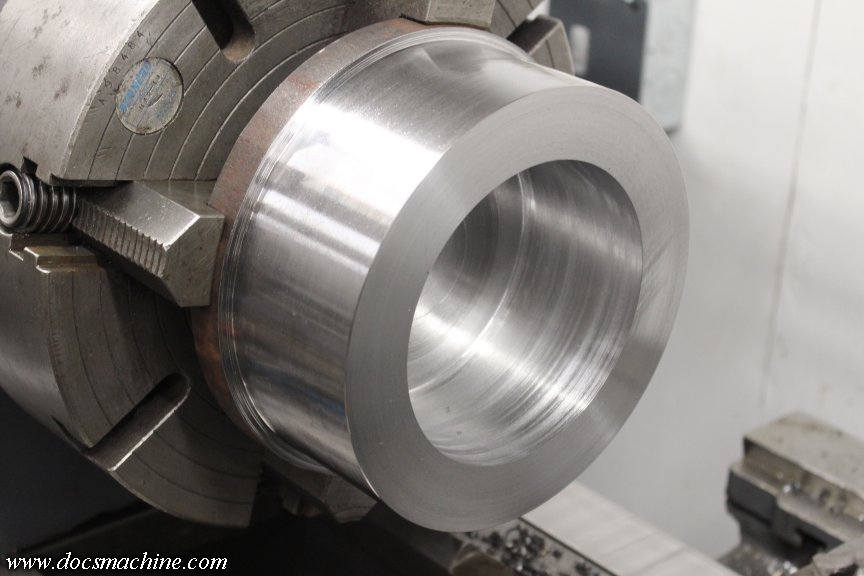
    And then, making roughly three hundred boring passes- in both senses of the word ...


    'Til it's mostly hollow.


    We're a long way from done, the wall thickness will eventually be around half an inch, but that was already about seven hours' work.

    And I have to do two of them.

    The white smoke? Vaporized WD-40. I was spraying a little in there basically just to reduce the chance of tip welding, but I'm not sure I was actually doing anything except filling the shop- and my lungs- with oil smoke. I don't have coolant on this machine, and this is one of those cases where I'd need heavy flood, or, well, don't bother.

    I don't really have an easy way to set it up at the moment, so basically, 'til we get down to the finish passes, we gotta do it dry. It's hard on the tools, but we don't have a lot of options.

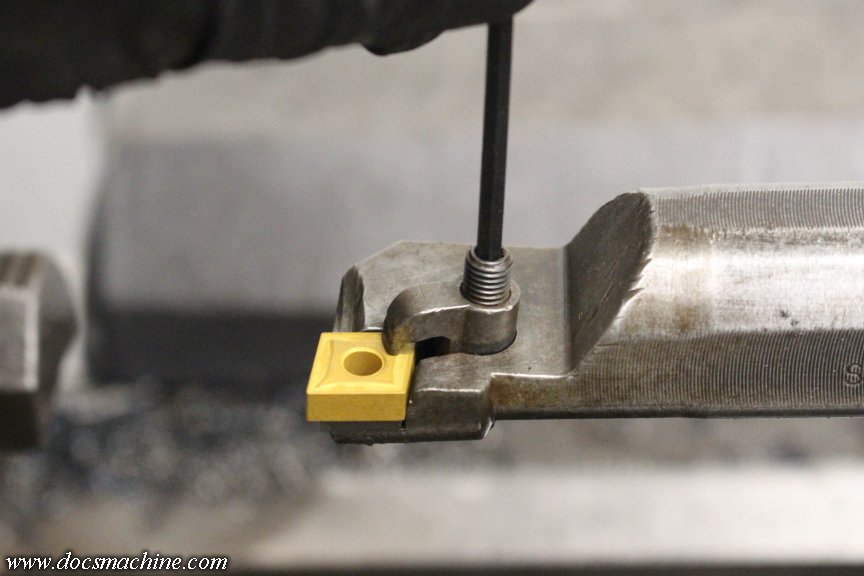
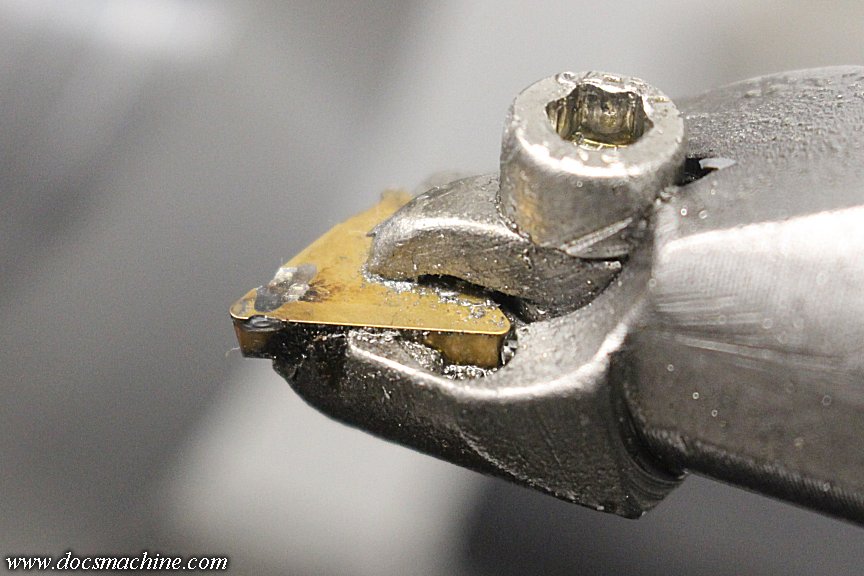
    The tools? I started that bore with a 3/4" shank boring bar, but I needed a bit more rigidity. This machine can take a substantial bite, and I had a lot of meat to move. The client loaned me a good- but worn- 1" shank boring bar, that added a good bit of beef. And I pushed those inserts for all they were worth.


    For those not familiar with tungsten carbide cutting inserts, the right-facing point of the gold bit is still new and untouched. The left facing point... those craters are worn. Those aren't chips or cracks, they're where the swarf come off the tip as it cuts, and scrubs past the insert.

    Why isn't the point itself worn? That is a very good question, and I'm not entirely sure I have a valid answer for that. I looked at the craters under magnification, and they clearly looked worn, not chipped. Why doesn't the cutting edge wear the same way? (Hey, I'm way more familiar with using the 'sharp honed' inserts on small bits of aluminum. )

    Oh, and the rear corner? That one's spalled- flaked off. That was probably thermal shock, most likely from when I sprayed in some WD-40 onto the 300°- 400°F insert.

    These need to be delivered on Monday, so I still have some work to do this weekend.

    Doc.​

    Leave a comment:


  • Pumps4ever
    commented on 's reply
    Well shit, I guess I was...

  • DocsMachine
    commented on 's reply
    Hangin' in my what? Are you confusing me with DocFire again?

    I'm still (checks underwear) Doc Nickel, of Doc's Machine, Alaska, and have been since 1998.

    Doc.

  • Pumps4ever
    commented on 's reply
    Kick ass Doc, was cool hangin in your live yesterday, Also super cool reminicing about the OG FPshooters!
Working...